Single/Double Stage Liquid
Ring Vacuum Pumps

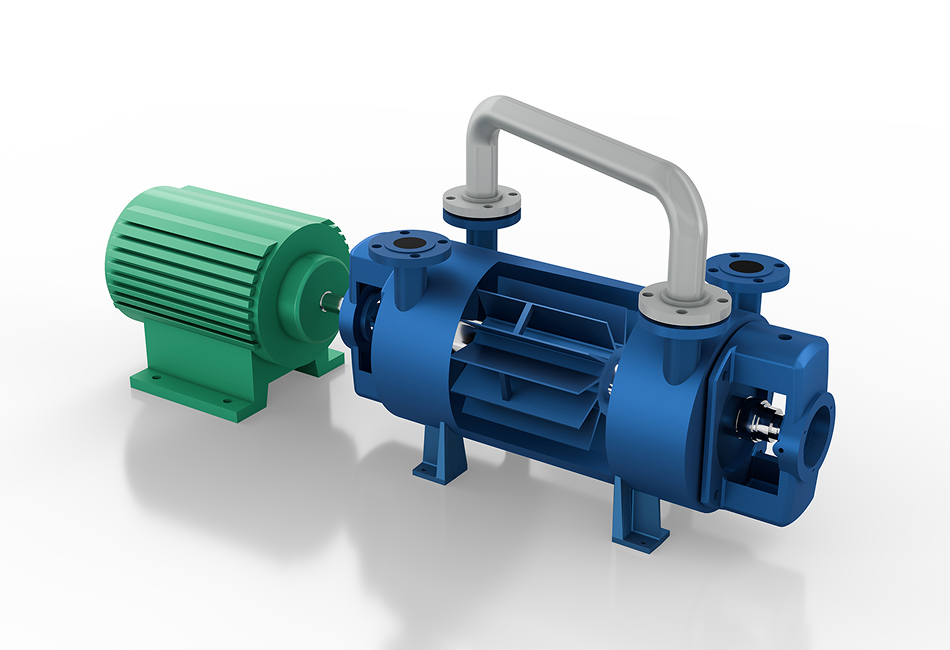
Mazda’s next-generation two-stage liquid ring vacuum pumps deliver superior efficiency, high reliability, and long-term energy savings.
Engineered with advanced design, they minimize operating costs while maximizing performance across diverse industrial applications.

Single/Double Stage Liquid
Ring Vacuum Pumps

Optimized vacuum technology designed for higher efficiency and lower power consumption.
Proven performance with robust construction for long-lasting service life.

Product Overview

Mazda’s two-stage liquid ring vacuum pumps represent a breakthrough in vacuum technology, offering operating efficiencies that reduce power consumption and extend motor life. These pumps achieve higher vacuums and capacities at reduced energy usage, making them one of the most economical and reliable solutions in the market. By combining advanced design with decades of expertise, Mazda ensures consistent, low-maintenance operation even in demanding industrial environments. With features such as combination air ejector options, these pumps can achieve lower suction pressures than conventional systems, protecting against cavitation and ensuring stable performance.

Advantages

  • Higher vacuum and capacity at reduced power consumption
  • Long-term operational cost savings
  • Reliable performance with stable operation
  • Protection against cavitation
  • Low maintenance and durable design
Single/Double Stage Liquid Ring Vacuum Pumps

Product Overview

Mazda’s two-stage liquid ring vacuum pumps represent a breakthrough in vacuum technology, offering operating efficiencies that reduce power consumption and extend motor life. These pumps achieve higher vacuums and capacities at reduced energy usage, making them one of the most economical and reliable solutions in the market. By combining advanced design with decades of expertise, Mazda ensures consistent, low-maintenance operation even in demanding industrial environments. With features such as combination air ejector options, these pumps can achieve lower suction pressures than conventional systems, protecting against cavitation and ensuring stable performance.

Advantages

  • Higher vacuum and capacity at reduced power consumption
  • Long-term operational cost savings
  • Reliable performance with stable operation
  • Protection against cavitation
  • Low maintenance and durable design

Ambient air enters through the motive air inlet and is accelerated by a venturi nozzle. This high-velocity jet entrains gases or vapors, which are then compressed and discharged into the liquid ring vacuum pump. The pump further compresses the mixture, ensuring efficient evacuation while maintaining stable operation across varied conditions.

Power Generation

Efficient vacuum generation for condenser and steam-cycle applications.

Chemical Processing

Reliable vacuum for demanding process applications involving gases and vapors.

Pharmaceuticals

Stable vacuum for controlled pharmaceutical processing applications.
Food & Beverage

Reliable vacuum for food and beverage processing operations.

Pulp & Paper

Dependable vacuum performance for continuous industrial processes.

Water Treatment & Utilities

Stable vacuum for water treatment and utility applications.

For any inquiries or assistance, our team is ready to offer professional support and guidance. Reach out to us, and we will respond promptly to meet your needs.

Request a Demo – Share Your Info
